Precision-Crafted CE Compliant Bikini Reference Designs
Explore production-tested silhouettes formulated for rapid customization, structural resilience in hyper-saline and chlorinated environments, and premium brand scalability.
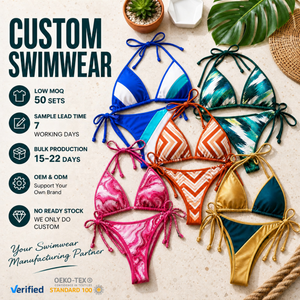
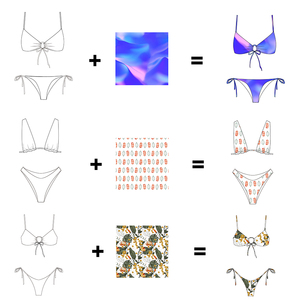
Deconstructing CE Compliance in High-Performance Swimwear Manufacturing
In global luxury and active swimwear supply chains, CE compliance and EU regulatory alignment (Regulation EU 2016/425, REACH Annex XVII, and EN 13758-1) represent the dividing line between fast-fashion liability and tier-one retail readiness.
REACH Annex XVII & Chemical Safety
Direct-to-skin marine textiles demand rigorous toxicology profiles. Under our quality assurance protocol, all virgin and recycled fibers pass testing for over 200 restricted substances, preventing heavy metal migration, carcinogenic arylamines from AZO dyestuffs, and phthalate plasticizers in heat transfers.
- Zero Nickel Release (EN 1811) on metallic sliders & clasps
- APEO / NPEO free non-hazardous wet-processing chemistry
- pH stabilization (4.5–7.5) adhering strictly to ISO 3071
Photoprotection Standard EN 13758-1/2
For swimwear marketing UV protection within the European Union, CE classification mandates verified spectrophotometric analysis. We employ dense micro-filament knitting matrices yielding UPF 50+ blocking efficiency (>98% UV radiation absorption) without reliant topical chemical washouts.
- Inherent mechanical fiber barrier retaining UPF post-wash
- Dual-wet/dry stretch spectrum UV testing verification
- Verified European PPE category 1 conformity documentation
Dynamic Hydro-Durability & Colorfastness
Bikini construction integrity is evaluated under accelerated degradation cycles: immersion in 50mg/L active chlorinated pool water (ISO 105-E03), synthetic perspiration (ISO 105-E04), and synthetic sea water (ISO 105-E02). We utilize high-tenacity Xtra Life Lycra® and bonded polyether urethane threads.
- Grade 4-5 Colorfastness rating against rub, sea salt & pool chemicals
- 4.5x greater resistance to fiber thinning and bagging vs ordinary elastane
- Overlocked 4-thread flatlock stitching maintaining 220% elongation
Macro Shifts in Global Swimwear Sourcing & Manufacturing Architecture
Procurement directors and direct-to-consumer label founders face evolving regulatory landscapes, circular economy mandates, and compressed go-to-market cycles. Here is how modern brands stay ahead.
1. Regenerated Polymers Replacing Virgin Polyamide
Global procurement benchmarks have shifted from optional sustainability to mandatory verifiable circularity. Tier-one fashion houses are dropping petrochemical nylon for certified regenerated yarns such as ECONYL® nylon (reclaimed from ghost fishing nets and industrial carpet scraps) and REPREVE® recycled PET sourced from post-consumer bottles.
2. Digital Product Passports (DPP) & Supply Chain Traceability
Driven by the European Green Deal and ESPR (Ecodesign for Sustainable Products Regulation), swimwear manufacturers must ensure complete provenance transparency. Every batch leaving our production studio carries verifiable chain-of-custody data, detailing raw polymer extraction, mill coordinates in Italy, dye lot toxicology, and carbon footprint metrics.
3. Ultra-Agile Micro-Batching & Inventory De-Risking
The era of rigid 5,000-unit minimum orders per SKU is over. Sustainable brand growth relies on lean inventory models. By deploying computer-aided digital marker cutting (saving up to 50% paper and minimizing fabric scrap) and split order structures (300 units distributed across up to 6 custom styles), brands can launch multi-color capsules with zero capital dead-stock exposure.
4. Size Inclusivity & Biomechanical Fit Engineering
Generic mathematical scaling across swimwear sizes leads to severe fit distortion in fuller busts and plus sizes. The modern standard demands fit-model validation across diverse body shapes (Petite, Tall, Maternity, Fuller Bust 30D–38G). Our digital pattern library covers XXS through XXL with customized underbust cradle reinforcement and load-distributing strap architecture.
5. High-Modulus Jacquards, Ribs & Dimensional Textures
Solid flat tricot knits are yielding ground to textured surfaces: 3D crinkle fabrics, engineered ribs, honeycomb knits, and fine lurex accents. These tactile surfaces not only provide an elevated visual identity and concealing compression but also exhibit superior resistance to sand entrapment and tensile recovery fatigue over multiple seasons.
6. Hybrid Active-Swim Functionality (Swim-to-Gym)
Boundary dissolution between water-sports performance, wellness, and beachwear is accelerating. Buyers are requesting multi-functional bikini silhouettes that double as sports bras and athleisure crop tops. This necessitates hydrophobic rapid-drying weaves, high-denier four-way stretch interlocks, and chlorine-proof internal elastic bands capable of enduring sweat and sun cream oils alike.
Comparative Procurement Matrix: Factory Archetypes
A rigorous breakdown showing why ethical, end-to-end studio production eliminates the hidden costs and compliance failure rates common in conventional offshore commodity sourcing.
| Evaluation Parameter | Our Ethical Production Studio | Conventional Commodity Overseas Factories | Trading Intermediaries / Sourcing Agents |
|---|---|---|---|
| MOQ Flexibility | 300 units total, split across up to 6 styles (50 pcs/style) | 1,500 – 3,000 units minimum per style/colorway | 500 – 1,000 units with added markups and split premiums |
| Regulatory & CE Testing | Full CE 2016/425, REACH Annex XVII & UPF 50+ compliance verified | Self-declared or non-verifiable test reports; high seizure risk | Variable, dependent on subcontracted third-tier facilities |
| Fabric Lineage | 100% Traceable Italian Carvico, Jersey Lomellina & ECONYL® | Generic, unverified polyester/spandex blends; high microplastic shedding | Re-badged market tricot lacking authenticated mill certificates |
| Pattern & Fit Development | In-house bespoke blocks, toiling, digitizing and sizing (XXS–XXL) | Basic manual scaling; significant fit distortions in plus/fuller cup sizes | Subcontracted out; 3–4 slow sample loops causing launch delays |
| Environmental Ethics | Digital zero-waste marker cutting, recycled packaging, green powered | High waste ratio, toxic dyeing baths, speculative bulk overproduction | No direct oversight on factory labor practices or energy footprint |
Integrated Studio Capabilities: From Concept to Global Distribution
Unlike outsourced brokers, we unite pattern design, fabric mills sourcing, physical toiling, computer grading, and bulk CMT production under one synchronized technical roof.
Technical Consulting & Critical Path
We review your tech packs, sketches, or reference samples, formalizing budget frameworks, yield computations, seam architecture, and strict critical-path launch timelines.
Precision Patterns & Physical Toiling
Our master pattern cutters draft bespoke production blocks. Fit prototypes (toiles) are cut and fit-adjusted on live technical models before expensive bulk fabric cutting begins.
Sublimation, Screen & Digital Printing
Advanced low-water digital disperse and reactive printing systems render razor-sharp motifs, custom engineered prints, and precise placement graphics on recycled polyamide fabrics.
CMT Bulk Assembly & AQL 2.5 Inspection
Dedicated industrial flatlock, zig-zag, and overlock operators assemble each piece under strict tension controls. Garments undergo 100% inline and end-line AQL 2.5 defect inspections.
Frequently Asked Questions for Sourcing & Production Directors
Detailed technical, compliance, financial, and logistical insights to streamline your bikini production lifecycle.
What specific CE documentation and testing certifications do you provide with bulk shipments?
How does your 300-unit minimum order quantity (MOQ) split across styles, sizes, and colors?
What is the realistic critical path lead time from initial tech pack review to warehouse delivery?
• Pattern drafting and initial toiling: 4–5 weeks (incorporating sampling fabric dispatch).
• Physical sample fabrication & live-model fitting: 2–3 weeks.
• Production grading and technical card preparation: 2–3 weeks (bulk yarn extrusion/milling initiated in parallel).
• Bulk CMT production, trim attachment & AQL 2.5 final inspection: 4–8 weeks.
If you choose our pre-developed, fit-tested Ready Designs catalogue, the development phase is skipped, reducing your turnaround to approximately 10 to 14 weeks from sign-off to ex-factory dispatch.
Can we supply our own custom hardware, metal tags, and custom branded packaging?
How do you engineer chlorine and sunscreen resistance into thin, delicate micro-bikinis?
What sustainability measures operate on your factory cutting room floor?
Build Your CE-Compliant Swimwear Line With Engineering Precision
Consult with our senior technical apparel specialists today. Receive comprehensive fabric swatch books, review our private label ready catalog, or submit your custom tech packs for detailed costing analysis within 24 business hours.